Ribbon Blender Working Principle: Convective Powder Blending Guide
In bulk solid processing and industrial formulation, achieving rapid batch homogeneity across ingredients with varying bulk densities remains a core engineering challenge. Các ribbon blender working principle delivers robust convective and shear mixing through a dual-spiral agitator mechanism.
Drawing upon 20 years of non-standard powder machinery manufacturing at JSCSTECH, we have supplied custom ribbon mixers to food seasoning, pharmaceutical excipient, dry mortar, and chemical pigment producers worldwide. Our design achieves coefficient of variation ($CV$) values below 3% ĐẾN 5% within 3 ĐẾN 10 minutes of cycle time.
A comprehensive understanding of the ribbon blender working principle allows process engineers to select appropriate ribbon pitch ratios, optimize drive power, and prevent material segregation during discharge. Here is our engineering breakdown of its mechanics, selection parameters, and design checks.

How Counter-Directional Helical Ribbons Generate 3D Convective Flow
The ribbon blender features a horizontal U-shaped trough fitted with a central shaft that supports inner and outer helical ribbon agitators. These ribbons are precisely engineered with opposing pitch angles to propel powder masses in opposite axial directions.
As the central shaft rotates at typical tip speeds of 1.0 ĐẾN 2.5 bệnh đa xơ cứng, the outer helical ribbon sweeps powder from the vessel sidewalls and ends toward the center discharge port. Đồng thời, the inner ribbon forces powder outward from the center toward the vessel ends.
This counter-directional axial movement combines with radial tumbling along the vessel curvature, creating a rapid three-dimensional convective blending pattern. Under the ribbon blender working principle, minor active ingredients and trace additives disperse uniformly throughout the bulk matrix without hot spots.
Key Design Factors Influencing Mixing Uniformity and Cycle Times
Optimizing mixing uniformity requires balancing vessel fill volume, ribbon clearance, and rotational velocity. The optimal working volume for horizontal ribbon blenders is between 40% Và 70% of total vessel capacity, allowing sufficient headspace for material expansion.
Tight mechanical clearance between the outer ribbon edge and the U-trough wall—ideally maintained between 2.0 mm and 4.0 mm—is vital for preventing static dead zones. For sanitary food and pharmaceutical applications, JSCSTECH machines the vessel with mirror-polished surfaces down to Ra ≤ 0.4 mm.
When formulations require liquid addition, such as spraying fats, binders, or liquid aromas onto dry powders, top-mounted atomizing spray manifolds distribute micro-droplets directly into the high-shear fluidized zone. This controlled atomization prevents wet agglomeration and produces consistent powder granules.
Drive Sizing and Power Calculations for High-Density Formulations
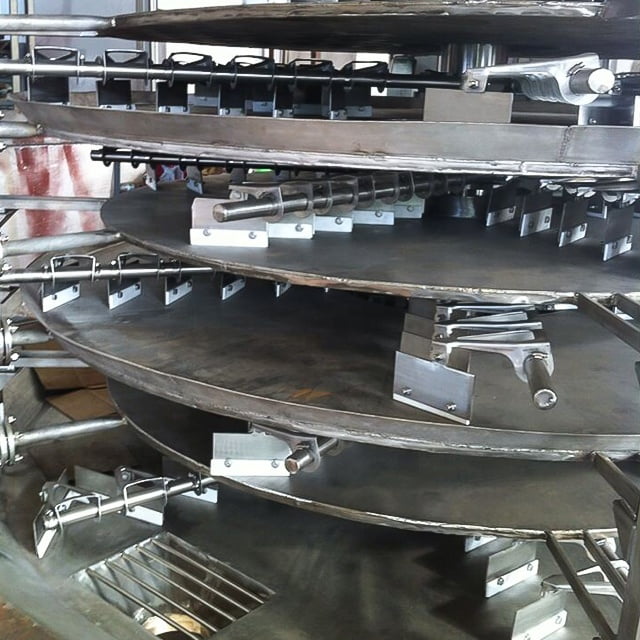
Sizing the electric motor and heavy-duty planetary or helical gearbox requires evaluating bulk material density, internal friction angle, and start-under-load torque requirements. Accurate motor sizing protects transmission gears against sudden torque spikes.
Standard drive power calculations incorporate effective torque coefficients through the relation $$P = \frac{T \cdot n}{9550 \cdot \eta}$$. Đây, $P$ is motor power (kW), $T$ is calculated operating torque (N·m), $n$ is rotational shaft speed (vòng/phút), and $\eta$ represents mechanical transmission efficiency.
At our manufacturing plant, we equip heavy-load ribbon blenders with variable frequency drives (VFD) and soft-start mechanisms. This protects mechanical seals and gear teeth from shock loading when starting with dense materials such as metal powders or wet mortar pastes.
Ribbon Blender vs. Tumbling Mixers and High-Shear Blenders
Selecting between convective ribbon blenders and rotating tumbling blenders depends on batch volume, shear sensitivity, and cleaning frequency requirements. Understanding these trade-offs ensures that plant operators choose the most cost-effective mixer type.
| Mixer Type | Ribbon Blender | Máy trộn V / Blender | Double Conical Mixer |
|---|---|---|---|
| Agitation Mechanism | Fixed Trough + Dual Helical Ribbons | Tumbling V-Chamber Geometry | Tumbling Symmetrical Cone |
| Typical Cycle Time | 3 – 10 Minutes (High Convection) | 10 – 25 Minutes (Dịu dàng) | 12 – 30 Minutes (Dịu dàng) |
| Shear Level | Moderate to High Shear | Low Shear (Non-destructive) | Low to Moderate Shear |
| Liquid Injection | Xuất sắc (Direct spray manifolds) | Giới hạn (Requires intensifier) | Giới hạn |
| Batch Volume Range | 100 L to 20,000+ L (quy mô lớn) | 50 L to 4,000 L | 100 L to 6,000 L |
| Discharge Cleanout | Pneumatic Bottom Flap Valve | Direct Bottom Butterfly Valve | Direct Bottom Butterfly Valve |
Process Integration and Powder Line Optimization
Ribbon blenders serve as foundational blending units in bulk powder production lines, pairing seamlessly with upstream bag dump stations and downstream pneumatic conveying systems. Review our complete thiết bị trộn công nghiệp range for high-capacity batch solutions.
For fragile, shear-sensitive granules requiring gentle tumbling, review our V mixer working principle guide and our square cone mixer working principle Phân tích. To establish quality control protocols, study our powder mixing uniformity testing guide.
For academic research on convective powder mechanics and granular flow velocity distributions, consult ScienceDirect ribbon blender granular flow analysis. These scientific publications provide empirical data on particle trajectory modeling.
Danh sách kiểm tra kiểm tra nhà cung cấp: 5 Documents to Request Before Ordering a Ribbon Blender
Prior to finalizing a commercial procurement contract for an industrial ribbon mixer, insist on obtaining the following 5 critical quality assurance and engineering verification documents from your equipment manufacturer. These documents safeguard plant operations against mechanical failures.
- Shaft Deflection & Finite Element Analysis (FEA) Report: Proves that central shaft deflection remains under 0.8 mm under 100% full-load torque.
- Ribbon-to-Trough Clearance Measurement Sheet: Validates laser-calibrated 2.0 ĐẾN 3.5 mm radial tolerances across the entire vessel trough.
- Material Mill Test Certificates (MTC EN 10204 3.1): Certifies food-grade SS304 or SS316L stainless steel composition for contact surfaces.
- Air-Purge Shaft Seal Leakage Test Certificate: Confirms zero powder ingress into bearing housings under continuous pressurized operation.
- Kiểm tra nghiệm thu tại nhà máy (MẬP) Run Protocol: Records vibration analysis, temperature rise curves, and full-load discharge valve sealing tests.
Frequently Asked Questions About Industrial Ribbon Blenders
Q1: What is the recommended filling level for a horizontal ribbon blender?
The optimum working level is 40% ĐẾN 70% of total vessel capacity, ensuring powder submerged above the outer ribbon apex while retaining expansion headspace. Tại CTCPSTECH, we calibrate ribbon pitch angles to prevent material surging and ensure uniform axial turnover. Always verify that supplier volumetric ratings reflect working volume rather than total geometric volume.
Q2: How can we prevent powder cross-contamination between product changeovers?
Cross-contamination is prevented by utilizing full-opening cantilevered covers, mirror-polished contact surfaces (Ra ≤ 0.4 mm), and flush-bottom contoured discharge flap valves that eliminate dead pockets. We also engineer sanitary air-purge split-packing shaft seals that disassemble quickly for complete washdown. Request CIP spray ball layout validation from your equipment manufacturer.
Q3: Can a ribbon blender effectively incorporate liquid additions into dry powders?
Đúng, horizontal ribbon blenders excel at liquid injection when equipped with pressurized atomizing spray nozzles mounted along the vessel top cover. The counter-helical agitation continuously turns over fresh dry powder directly beneath the spray zone, preventing clumping and agglomeration. Verify that liquid delivery pumps synchronize with agitator speed controls.
Contact Our Engineering Team via WhatsApp: +86 137 7529 9712